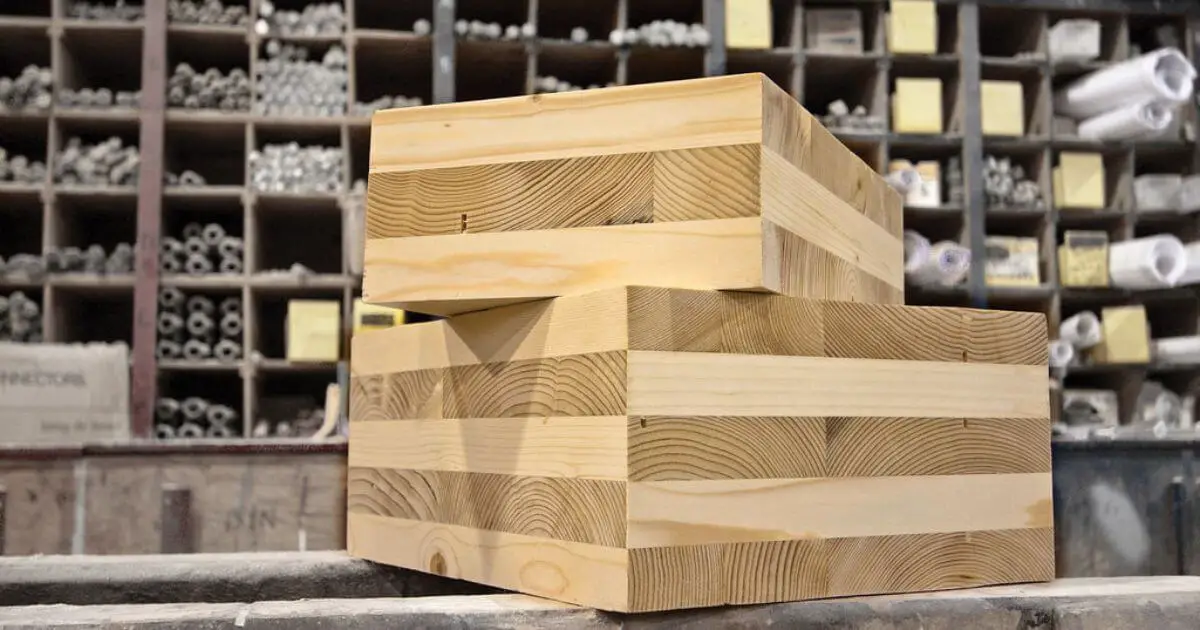
Cross-laminated timber (CLT) is made by bonding layers of dried, strength-graded lumber, usually with adjacent layers arranged at right angles. The assembled layers are pressed until the adhesive develops the required bond, then machined into building components.
Unlike plywood, which uses thin veneers, CLT uses boards to create thick structural panels. These panels can form load-bearing walls, floors, and roofs, with exposed undersides sometimes serving as finished ceilings.
The manufacturing process involves much more than stacking boards and adding glue. Moisture control, lumber grading, surface preparation, and bond quality all affect the finished panel’s performance.
For a broader introduction, read our guide to cross-laminated timber.
CLT Manufacturing Process at a Glance
A typical production sequence is:
Lumber supply → drying → grading → cutting and finger-jointing → planing → adhesive application and lay-up → pressing and curing → machining and inspection → delivery
The exact order and equipment vary between factories. Quality checks take place throughout production, rather than only at the end.
1. Selecting and Preparing the Lumber
CLT production begins with suitable sawn lumber. Some manufacturers operate alongside sawmills, while others purchase boards that have already been sawn, dried, and graded.
Where logs are processed on-site, they are debarked and sawn into boards before lumber drying. Debarking removes the outer bark; it does not prepare the bonding surfaces of the finished boards.
Spruce, pine, and fir are common raw materials. Other species may be used where they are covered by the manufacturer’s qualified product specification.
Species selection depends on availability, mechanical properties, adhesive compatibility, and the intended panel grade.
2. Kiln-Drying and Moisture Checks
The boards are kiln-dried to a controlled moisture range suitable for bonding and the finished product.
A kiln regulates temperature, humidity, and airflow to remove moisture. The aim is not to remove all water from the wood, but to achieve an appropriate, reasonably consistent moisture content.
This matters because differences in moisture between boards can contribute to movement and internal stresses. Moisture also affects how some adhesives cure.
As a product-specific example, Nordic’s published X-Lam technical data lists a moisture content of approximately 12% ± 2%. Manufacturers establish their own permitted ranges under the applicable specification; one figure should not be treated as universal.
Boards outside the accepted range need further conditioning or must be removed from the production flow.
3. Strength Grading and Sorting
The lumber is assessed and sorted according to the requirements of the panel lay-up.
Grading may involve visual inspection, machine assessment, or both. Relevant characteristics include knots, grain deviation, defects, and stiffness.
The manufacturer then assigns suitable lumber to particular layers. Different layer positions may have different structural requirements.
Appearance grade and structural grade are separate considerations. A board selected for a visible ceiling surface may have stricter cosmetic requirements, but an attractive surface alone does not establish its load-bearing capacity.
4. Cutting Out Defects and Finger-Jointing
Boards are cut to remove unacceptable defects and produce suitable lengths.
Where longer laminations are needed, shorter pieces may be joined end-to-end using structural finger joints. Matching finger-shaped profiles are machined into the board ends, adhesive is applied, and the joint is pressed.
Finger-jointing helps manufacturers produce consistent lengths while using shorter pieces efficiently. However, not every board in every CLT product must be finger-jointed.
The joints must meet the relevant production and quality requirements; they are not simply ordinary woodworking joints added for convenience.
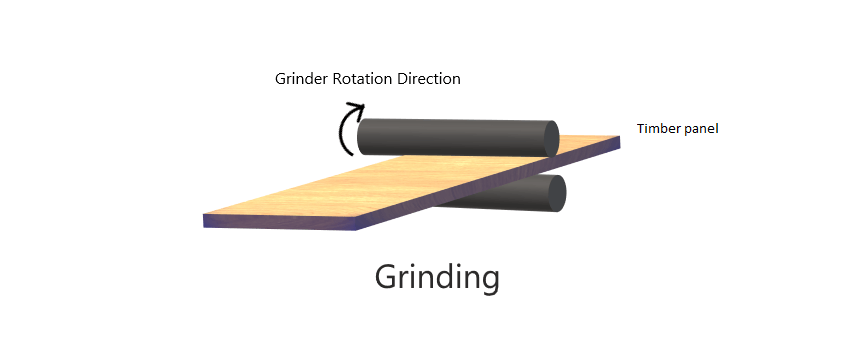
5. Planing the Bonding Surfaces
The laminations are planed to achieve the required thickness and prepare their surfaces for bonding.
Accurate machining helps adjacent layers make close contact. Uneven surfaces, contamination, or unsuitable tolerances can interfere with adhesive performance.
This step is better described as planing and surface preparation, rather than grinding the lumber with sandpaper. Sanding may be used later for appearance, but it is not a universal substitute for preparing structural bond surfaces.
Modern production equipment can integrate sorting, finger-jointing, planing, adhesive application, and pressing into one coordinated line. Ledinek’s CLT production overview illustrates these manufacturing stages.
6. Applying Adhesive and Arranging the Layers
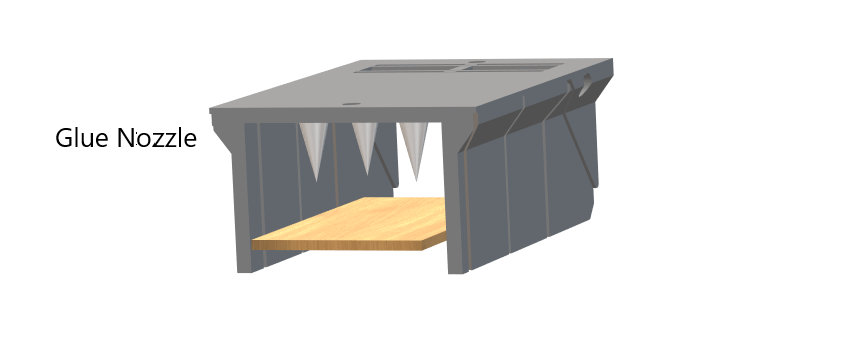
A controlled quantity of structural adhesive is applied to the prepared surfaces. The application method depends on the production line and adhesive system.
One-component polyurethane is used in some CLT manufacturing systems. Other qualified adhesive systems may also be used. Manufacturers must control factors such as spread rate, assembly time, and temperature according to the approved process.
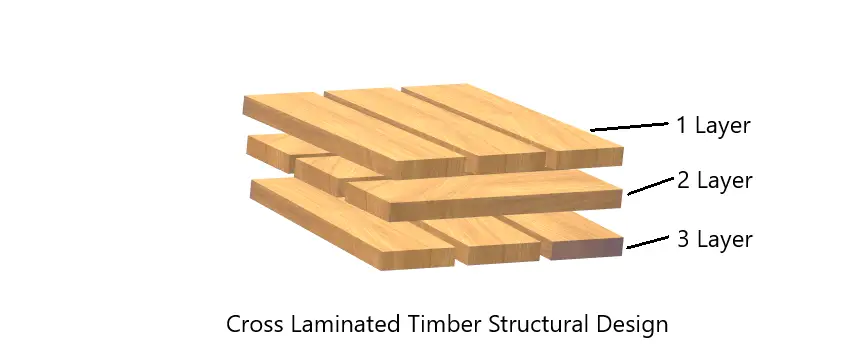
The boards are then arranged into layers following the specified panel design.
How Are CLT Layers Arranged?
A simple three-layer panel commonly has:
- A first layer running lengthwise.
- A second layer running across it.
- A third layer running lengthwise again.
Five- and seven-layer panels are also common. More complex lay-ups are possible, including designs with neighboring layers running in the same direction.
These are layers of boards, not three, five, or seven individual boards. Each layer generally contains several boards placed side by side.
Layer thicknesses do not have to be identical. Their dimensions, grades, and orientation are chosen to achieve the required panel performance.
7. Pressing and Adhesive Curing
The assembled panel enters a press, which holds the layers together while the adhesive develops sufficient bond strength.
Pressure helps maintain contact across the bonding surfaces. The required pressure and pressing time depend on the equipment, adhesive, and qualified manufacturing process.
Does CLT Require High-Temperature Pressing?
Not necessarily. Some production systems use cold-setting adhesives, so CLT manufacturing should not be described as universally requiring a hot press.
There is also no single temperature or pressure range suitable for every factory. The original figures of 100–150°C and 700–6,000 psi should not be presented as standard CLT manufacturing conditions.
Manufacturers use validated settings and observe any additional curing requirements before machining or handling the panels further.
8. CNC Machining and Quality Inspection
After sufficient curing, panels are trimmed and machined to the project dimensions.
Computer-controlled equipment can produce features such as:
- Door and window openings.
- Panel edges and connection recesses.
- Service penetrations.
- Specified drilling and lifting details.
Factory machining helps reduce cutting on-site, but it makes accurate design coordination important. Openings and connections should be agreed upon before production.
Additional cuts made later can affect structural performance and need appropriate review.
What Quality Checks Are Performed?
The quality-control program may include checks on lumber moisture, grading, finger joints, adhesive application, bond integrity, dimensions, and machining accuracy.
Depending on the applicable standard, representative samples undergo tests such as bond shear or delamination assessment. These checks evaluate whether production continues to meet the qualified requirements.
In North America, ANSI/APA PRG 320 provides requirements for performance-rated CLT qualification and quality assurance. The APA overview of CLT explains the product and links to the standard.
9. Labeling, Protection, and Delivery
Finished panels are identified so they can be traced to their production records and installed in the correct location.
Project panels are often organized for the planned erection sequence, then protected and transported to the construction site. CLT is commonly supplied through a manufacturer or project supplier rather than selected from ordinary retail stock.
Packaging helps protect the panels during transport, but moisture management must continue after delivery. Site storage, lifting arrangements, and weather protection should be planned before the truck arrives.
Inspection is also important: damage or wetting during transport should be identified before installation.
Why Are the Layers Cross-Laminated?
Wood behaves differently along and across its grain. Alternating the grain direction helps restrain movement within the panel and enables structural action in more than one direction.
However, CLT is not equally strong in every direction. Its performance depends on the layer arrangement, lumber properties, panel thickness, connections, and support conditions.
Cross-lamination also does not make the material waterproof or eliminate all swelling, shrinkage, and checking.
Is CLT Made the Same Way as Glulam?
Both products use graded lumber bonded with structural adhesive, but their usual arrangements differ.
CLT typically has cross-oriented layers and is used as a panel. Glulam generally has laminations running parallel and is commonly used for beams and columns.
They often work together in a building—for example, CLT floor panels supported by glulam beams.
Frequently Asked Questions
How Many Layers Does CLT Have?
CLT commonly has three, five, or seven layers, although other configurations are available. The required lay-up depends on the product and structural design.
Is CLT Waterproof Because It Contains Structural Adhesive?
No. A durable adhesive bond does not prevent the wood from absorbing moisture. CLT buildings still need appropriate weather protection, drainage, and moisture detailing.
Is CLT Always Made From Softwood?
Softwoods are common, but other species can be used in qualified products. Manufacturers cannot freely substitute species without considering the product’s approval and performance requirements.
Can CLT Be Made With Ordinary Wood Glue?
Building-grade CLT requires a qualified manufacturing process, suitable structural adhesive, and documented quality control. Gluing boards together in a workshop does not establish that the resulting panel is suitable for structural construction.
Are All CLT Panels the Same Size?
No. Available dimensions depend on the factory’s equipment, the qualified product range, transportation limits, and project requirements. Designers coordinate panel sizes with the manufacturer before production.